LINCOLN CHROMET92®
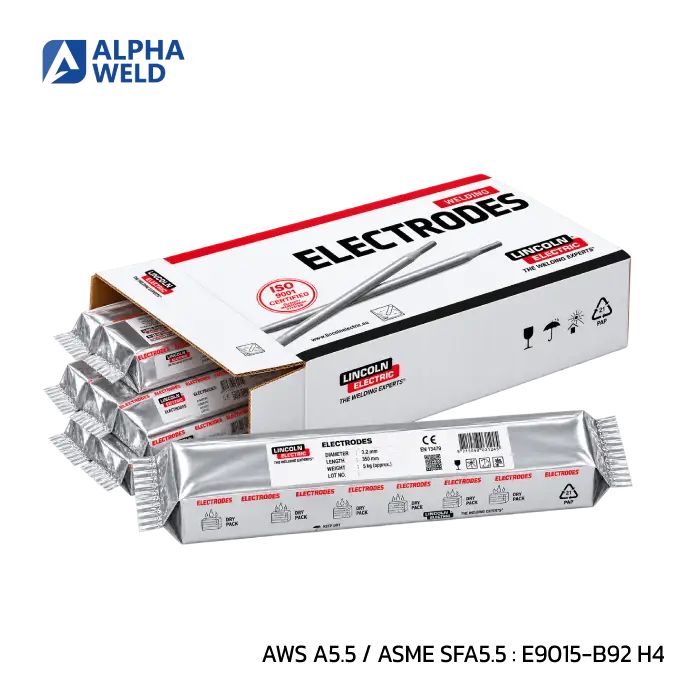
AWS A5.5 / ASME SFA5.5 : E9015-B92 H4
AWS A5.5 / ASME SFA5.5 : E9015-B92 H4
EN ISO 3580-A : E ZCrMoWVNb 9 0.5 B 3 2 H5
CHROMET® 92 is a low-hydrogen electrode designed for welding equivalent P92 modified 9Cr steels, offering high strength and improved long-term creep resistance at elevated temperatures. It provides excellent high-temperature structural performance and low weld metal hydrogen levels through its moisture-resistant coating. It is suitable for main steam piping, power generation plants, oil refineries, coal gasification plants, and turbine components.
Typical chemical composition of weld metal (wt%) | |||||||||
C | Mn | Si | S | P | Cr | Ni | Mo | W | Nb |
0.11 | 0.6 | 0.25 | 0.010 | 0.010 | 9.0 | 0.60 | 0.45 | 1.7 | 0.05 |
V | N | B | Al | Cu |
|
|
|
|
|
0.20 | 0.05 | 0.003 | <0.01 | <0.05 |
|
|
|
|
|
Sizes available and recommendation currents (AC or DCEP) | |||
Diameter (mm) | 2.5 | 3.2 | 4.0 |
Length (mm) | 350 | 350 | 350 |
Current (A) | 70 - 110 | 80 - 140 | 100 - 180 |
Typical mechanical properties of all-weld metal | ||||
Condition | Y.S. (MPa) | T.S. (MPa) | El. (%) | IV 20 °C (J) |
PWHT 2-4hr @ 760°C | 630 | 740 | 22 | 60 |
-