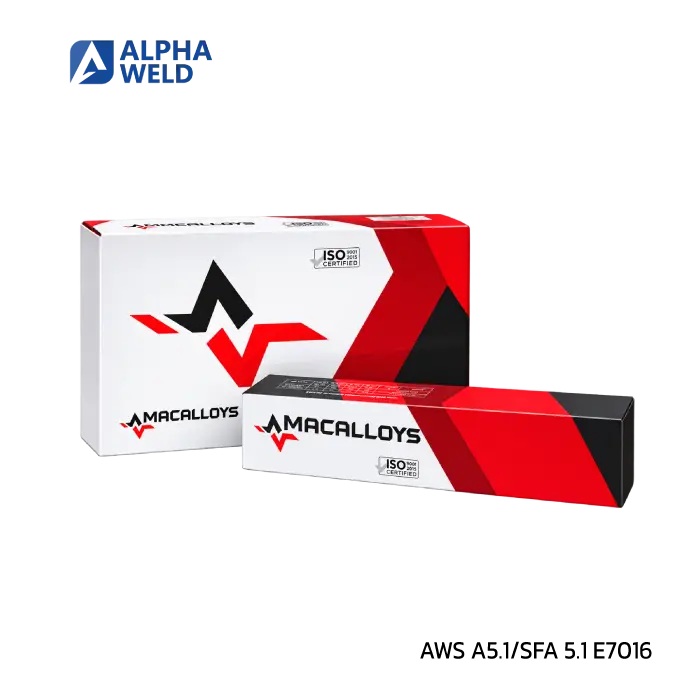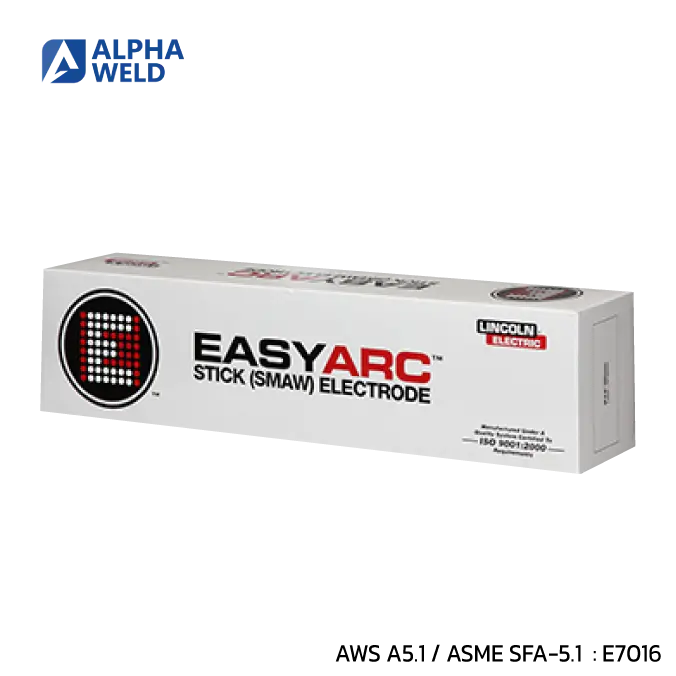
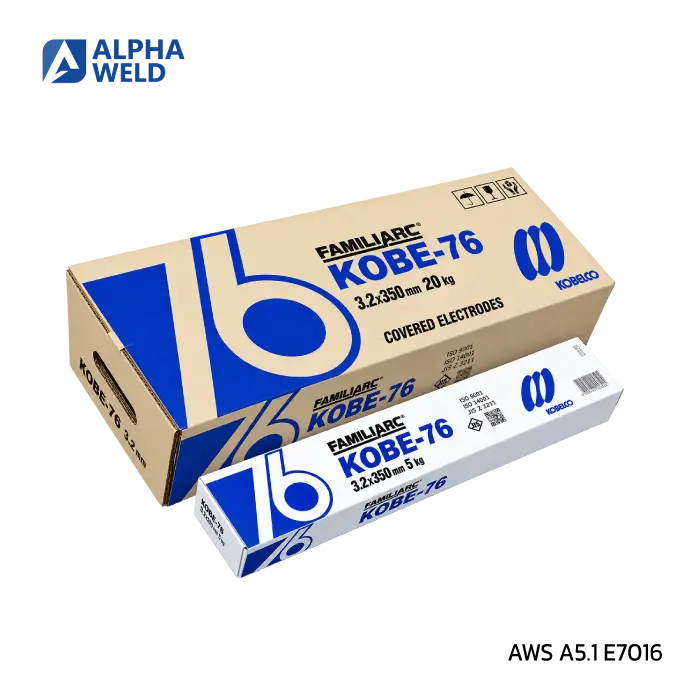
KOBE-76
AWS A5.1 : E7016
SMAW (MMA) CARBON STEEL
AWS A5.1 : E7016
KOBE-76 is a low hydrogen type covered electrode for welding mild steel and high tensile steel up to 490 MPa.
Easy to start arc and provides smooth arc.
There are few welding sparks and smoke.
Easy slag removability, smooth and flat shape beads with X-ray-quality
Application
Suitable for welding heavt steel plates and heavy steel structures that require high strength, including buffer welding before hard facing electrode in machinery maintenance work..
Typical chemical composition of weld metal (wt%) | ||||
C | Si | Mn | P | S |
0.08 | 0.58 | 1.27 | 0.009 | 0.001 |
Typical mechanical properties of all-weld metal | ||||
Condition | Y.S. (MPa) | T.S. (MPa) | El. (%) | IV -30 °C (J) |
AW | 498 | 603 | 32 | 180 |
Sizes available and recommendation currents (AC or DCEP) | |||||
Diameter (mm) | 2.6 | 3.2 | 4.0 | 5.0 | |
Length (mm) | 350 | 350 | 400 | 400 | |
Current (A) | F | 55 - 85 | 90 - 130 | 130 - 180 | 180 - 240 |
V & OH | 50 - 80 | 80 - 120 | 110 - 170 | 150 - 200 | |
Packaging (kg) | 5 | 5 | 5 | 5 | |
Carton (kg) | 20 | 20 | 20 | 20 | |
Approvals |
- |
Notes on usage: |
|
-