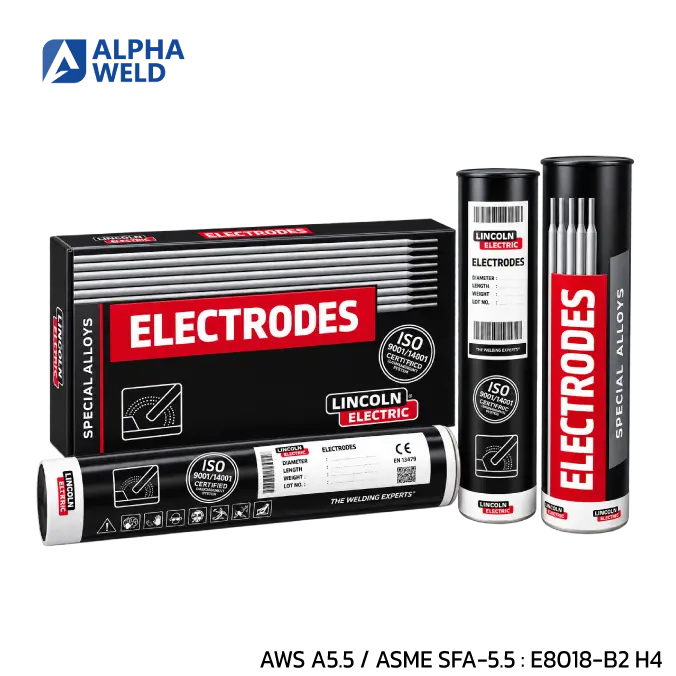
LINCOLN CHROMET® 1X
AWS A5.5 / ASME SFA-5.5 : E8018-B2 H4
AWS A5.5 / ASME SFA-5.5 : E8018-B2 H4
EN ISO 3580-A : E CrMo1 B 3 2 H5
Basic flux, metal powder type coatings on low carbon high purity core wire.
1¼Cr-½Mo deposit which meets specific requirements for improved temper embrittlement resistance
with prolonged service at 400-600°C.
Relevant trace elements (P, Sn, As, Sb) are controlled to ensure low Bruscato (X) and Watanabe (J) factors.
Application
MMA electrode meeting AWS and BS EN national standards suitable for most power generation applications, Petro-Chemical, Piping, Boiler Superheaters, Turbine Casting.
Typical chemical composition of weld metal (wt%) | |||||||||
C | Mn | Si | S | P | Cr | Mo | Cu | Sn | As |
0.06 | 0.70 | 0.25 | 0.012 | 0.009 | 1.25 | 0.55 | <0.05 | 0.002 | 0.003 |
*Mn+Si < 1.10% | |||||||||
Bruscato factor (X) : 10P + 5Sb + 4Sn + As (ppm)/100 = 15 Max | |||||||||
Watanabe factor (J) : (Mn+Si)x(P + Sn) x 104 = 180 max | |||||||||
Typical mechanical properties of all-weld metal | ||||
Condition | Y.S. (MPa) | T.S. (MPa) | El. (%) | IV +20 °C (J) |
PWHT 690°C/1h | 610 | 515 | 25 | 160 |
|
|
|
|
|
Sizes available and recommendation currents (DCEP) | |||||
Diameter (mm) | 2.6 | 3.2 | 4.0 | 5.0 | |
Length (mm) | 350 | 350 | 350 | 350 | |
Current (A) |
| 50 - 75 | 70 - 95 | 100 - 155 | 130 - 190 |
| |||||
-