LINCOLN CHROMET® 2X
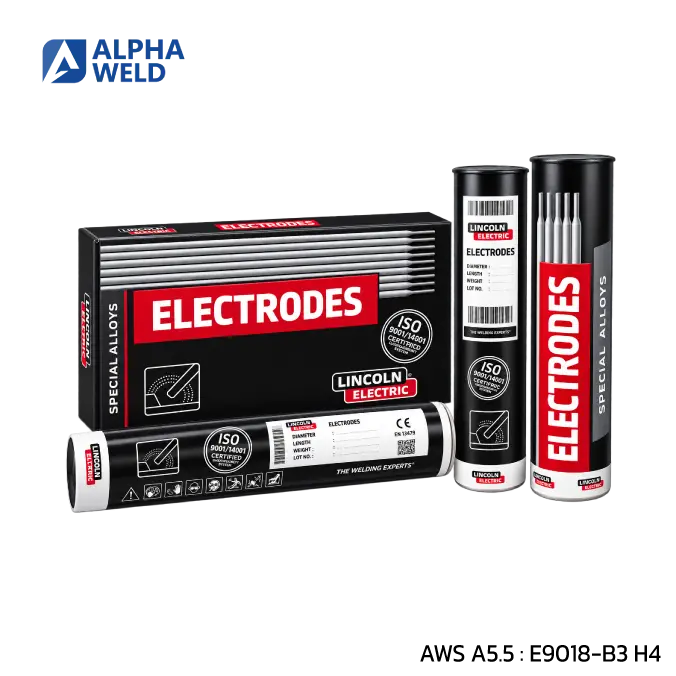
AWS A5.5 : E9018-B3 H4
AWS A5.5 : E9018-B3 H4
EN ISO 3580-A : E CrMo2 B 3 2 H5
BS EN ISO 3580-B: E 6216-2C1M
B3 alloyed steel: 2.25% chromium, 1% molybdenum deposit which meets specific requirements for improved temper embrittlement resistance with prolonged service at 400°C-600°C (752°F-1112°F)
Moisture resistant coating provides low amounts of weld metal hydrogen levels for a superior weld.
Weld metal chemistry is low in impurity elements allowing it to respect the X Factor (<15ppm) and J-factor (<120ppm)
Application
MMA electrode meeting AWS and BS EN national standards suitable for most power generation applications, Petro-Chemical, Piping, Boiler Superheaters, Turbine Casting.
Typical chemical composition of weld metal (wt%) | ||||
C | Si | Mn | P | S |
0.06 | 0.25 | 0.70 | 0.010 | 0.012 |
Sizes available and recommendation currents (AC or DCEP) | ||||||||||||||
Diameter (mm) | 2.5 mm (3/32 in) | 3.2 mm (1/8 in) | 4.0 mm (5/32 in) | 5.0 mm (3/16 in) | ||||||||||
Length (mm) | 350 | 350 | 450 | 450 | ||||||||||
Current (A) | 70 - 100 | 80 - 140 | 100 - 180 | 140 - 240 | ||||||||||
Typical chemical composition of weld metal (wt%) | ||||||||||||||
C | Mn | Si | S | P | Cr | Mo | Cu | Sn | As | |||||
0.06 | 0.70 | 0.25 | 0.012 | 0.009 | 1.25 | 0.55 | <0.05 | 0.002 | 0.003 | |||||
*Mn+Si < 1.10% | ||||||||||||||
Bruscato factor (X) : 10P + 5Sb + 4Sn + As (ppm)/100 = 15 Max | ||||||||||||||
Watanabe factor (J) : (Mn+Si)x(P + Sn) x 104 = 180 max | ||||||||||||||
Typical mechanical properties of all-weld metal | ||||
Condition | Y.S. (MPa) | T.S. (MPa) | El. (%) | IV -30 °C (J) |
PWHT 690°C/1h | 570 | 670 | 22 | 80 |
|
|
|
|
|
-