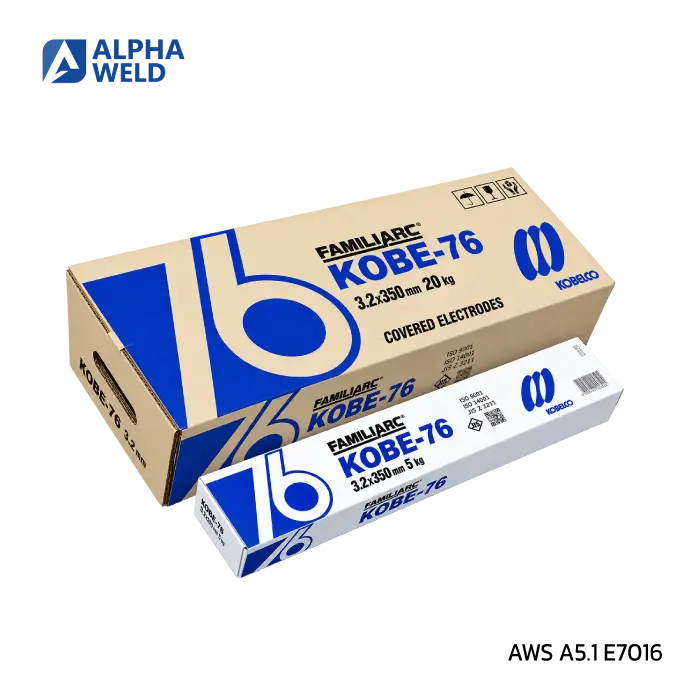
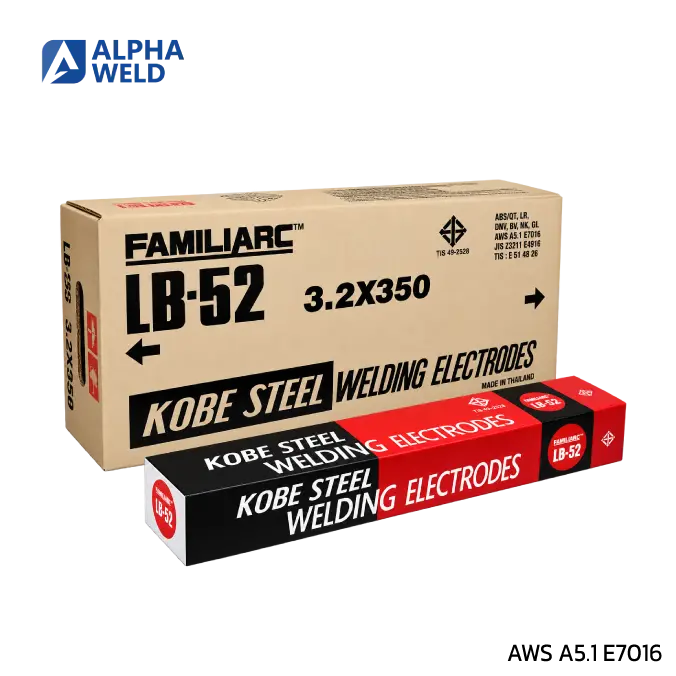
KOBE LB-52
AWS A5.1 : E7016
AWS A5.1 : E7016
JIS Z3211 E4916
TIS 49-B-E 49 16 A
LB-52 is a low hydrogen electrode widely used in all-position welding of 490 MPa high tensile steels.
LB-52 provides crack-resistant welds with excellent mechanical properties and X-ray quality.
Easy slag removability, smooth and a beautiful, uniform weld bead.
Application
Suitable for welding mild steel and 490 MPa high tensile steel in shipbuilding, bridges, buildings and pressure vessels.
Typical chemical composition of weld metal (wt%) | ||||
C | Si | Mn | P | S |
0.08 | 0.60 | 0.97 | 0.011 | 0.006 |
Typical mechanical properties of all-weld metal | ||||
Condition | Y.S. (MPa) | T.S. (MPa) | El. (%) | IV -29 °C (J) |
AW | 500 | 570 | 32 | 120 |
620 °C x 1 hr | 420 | 520 | 33 | 150 |
Sizes available and recommendation currents (AC or DCEP) | |||||
Diameter (mm) | 2.6 | 3.2 | 4.0 | 5.0 | |
Length (mm) | 350 | 350 | 400 | 400 | |
Current (A) | F | 55 - 85 | 90 - 130 | 130 - 180 | 180 - 240 |
V & OH | 50 - 80 | 80 - 120 | 110 - 170 | 150 - 200 | |
Packaging (kg) | 5 | 5 | 5 | 5 | |
Carton (kg) | 20 | 20 | 20 | 20 | |
Approvals |
- |
Notes on usage: |
|
-