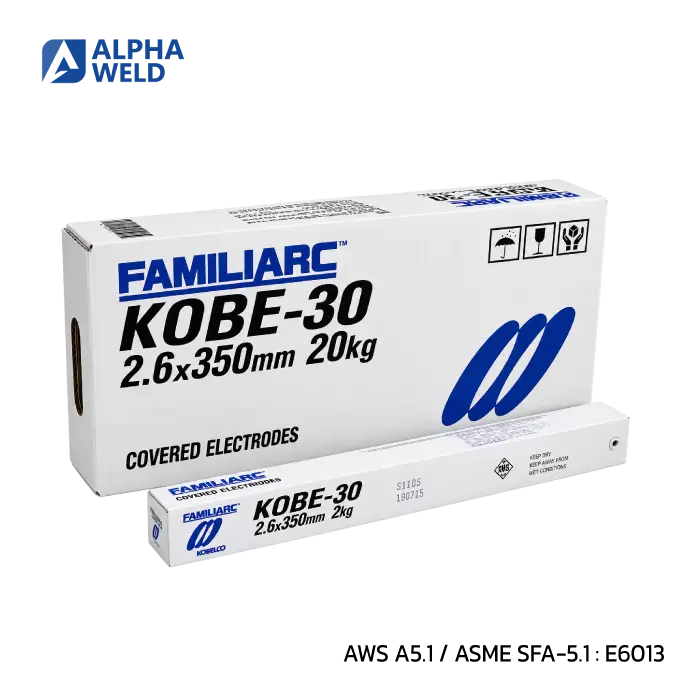
KOBE-30
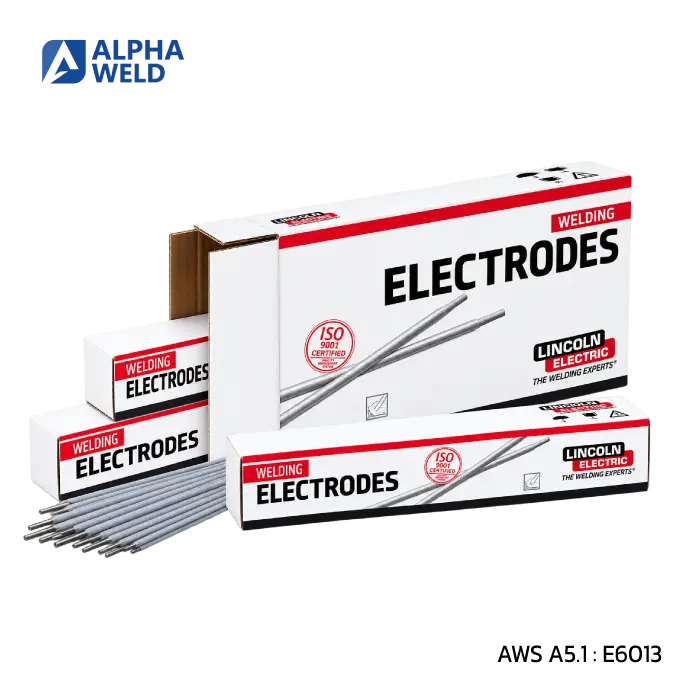
AWS A5.1 / ASME SFA-5.1 : E6013
SMAW (MMA) CARBON STEEL
AWS A5.1 / ASME SFA-5.1 : E6013
JIS Z3211 E4313
TIS 49-B-E 43 13 A
KOBE-30 is a high titania covered electrode that provides a strong and stable arc, enabling excellent welding in vertical and downward positions.
The weld surface is smooth and shiny. With good mechanical properties, easy slag removability
Application
Suitable for welding thin steel structures, thin steel plates in shipbuilding, railways and automobiles made of mild steel
Typical chemical composition of weld metal (wt%) | ||||
C | Si | Mn | P | S |
0.09 | 0.28 | 0.39 | 0.011 | 0.014 |
Typical mechanical properties of all-weld metal | ||||
Condition | Y.S. (MPa) | T.S. (MPa) | El. (%) | IV 0 °C (J) |
AW | 450 | 510 | 25 | - |
Sizes available and recommendation currents (AC or DCEP) | |||||
Diameter (mm) | 2.6 | 3.2 | 4.0 | 5.0 | |
Length (mm) | 350 | 350 | 400 | 400 | |
Current (A) | F | 45 - 95 | 60 - 120 | 105 - 170 | 150 - 220 |
V & OH | 45 - 95 | 60 - 125 | 100 - 150 | 125 - 190 | |
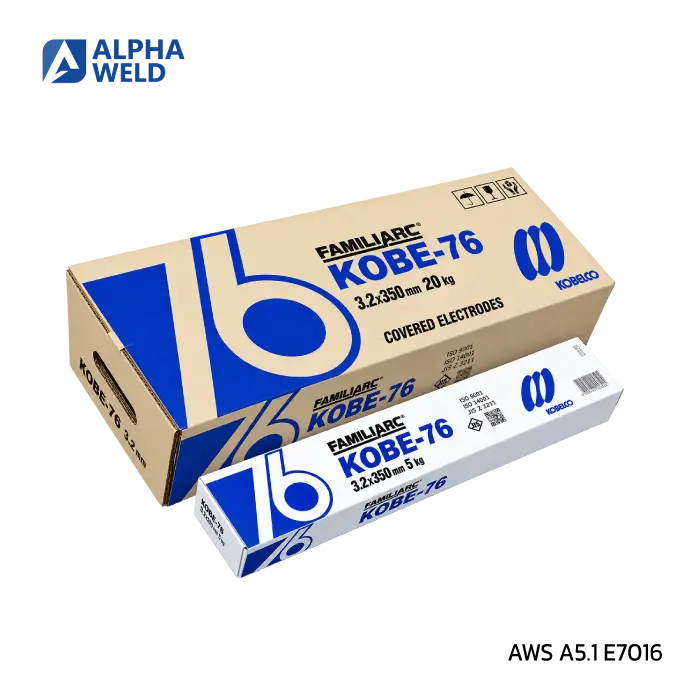
Packaging (kg) | 5 | 5 | 5 | 5 | |
Carton (kg) | 20 | 20 | 20 | 20 | |
Approvals |
JIS TIS |
Notes on usage: |
|
-