MACALLOYS MCT-NiCrMo-4
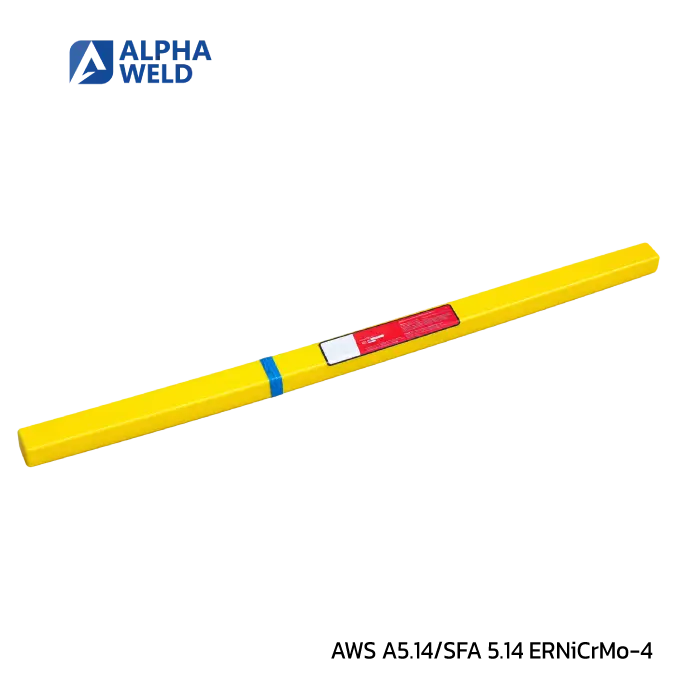
AWS A5.14/SFA 5.14 ERNiCrMo-4
AWS A5.14/SFA 5.14 ERNiCrMo-4 EN ISO 18274 S Ni 6276 (NiCr15Mo16Fe6W4)
JIS Z 3334 S Ni 6276 (NiCr15Mo16Fe6W4)
‣ Ni-Cr-Mo type argon gas welding wire for the welding of 9Ni steel, hastelloy C276 or dissimilar welding on the surface of
nickel alloys, low alloys, steels, and stainless steels.
‣ Suitable for welding components in plants for chemical processes with highly corrosive media, but also for surfacing press
tools, punches, etc. which operate at high temperature.
‣ Excellent pitting resistance and crevice corrosion resistance, especially for sulfuric acids at high chloride concentrations.
Base materials
‣ Alloy C276 UNS N10276, B575, B626
Typical chemical composition of weld metal (wt%) | |||||||||
C | Mn | Si | Cr | Ni | Mo | Fe | W | P | S |
0.01 | 0.50 | 0.04 | 15.88 | 58.10 | 15.75 | 5.60 | 3.57 | 0.001 | 0.001 |
Typical mechanical properties of all-weld metal | ||||
Condition | Y.S. (MPa) | T.S. (MPa) | El. (%) | IV -196 °C (J) |
AW |
| 785 | 40 | 90 |
Sizes available and recommendation currents (DCEN) | ||||
Diameter (mm) | 1.6 | 2.0 | 2.4 | 3.2 |
Length (mm) | 1000 | 1000 | 1000 | 1000 |
Current (A) | 80 - 120 | 100 - 130 | 130 - 160 | 160 - 200 |
Voltage (V) | 10 - 12 | 14 - 16 | 16 - 18 | 17 - 20 |
Packaging (kg) | 5 | 5 | 5 | 5 |
Notes on usage: |
|
-